Mechanical engineering and its industrialization is constantly evolving as new requirements emerge in the strategic sectors of Space, Nuclear & Energy, Defense and other hi-tech industries.
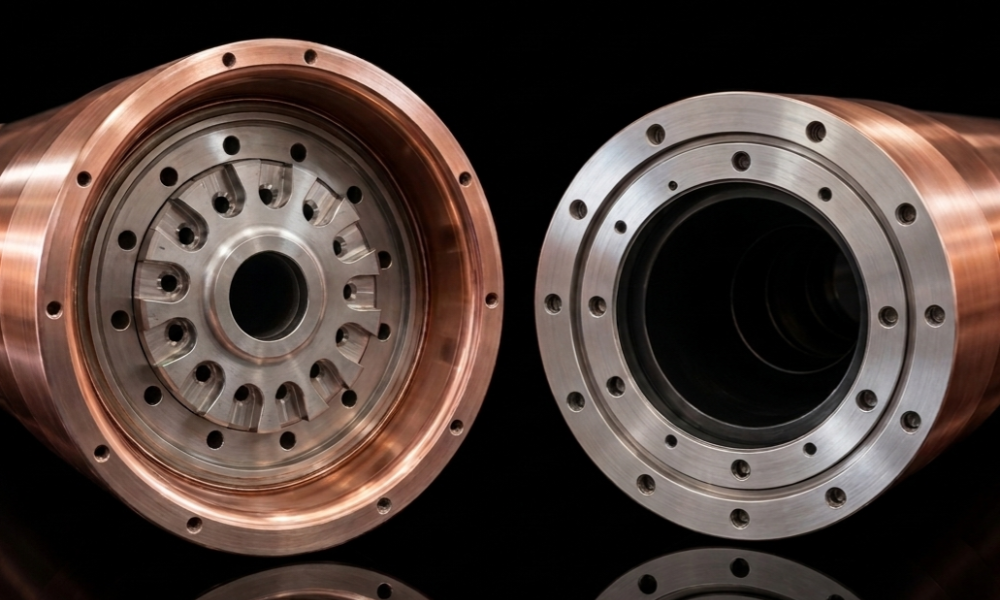
In close collaboration with research teams from the CEA and as part of strategic programs linked to the ITER Organization, Spirit Technologies provided the industrialization and manufacturing of a high-frequency resonator intended for a cutting-edge industrial nuclear project.
This critical component illustrates our mechanical engineering teams' ability to deliver complex equipment meeting the most demanding physical and thermal constraints of nuclear fusion and the energy sector.
High-Tech Industrialization for the Nuclear Sector
Developing this high-frequency resonator required advanced expertise in precision engineering, mechanical manufacturing, and environmental control:
Tailor-Made Design and Industrialization: Translating CEA research specifications into a repeatable, reliable industrial system compliant with ITER standards.
Mastery of Specialized Machining & Materials: Achieving sub-millimeter geometric tolerances and high-precision welded structures under severe operating conditions.
Specialized Partner Ecosystem: Coordinating expert partners for specific surface treatments and non-destructive testing to guarantee total component integrity.
Nuclear Safety & Reliability Requirements: Strict adherence to qualification protocols, cleanliness standards, and certification processes required for nuclear installations.
High-End Engineering Driven by Performance
This achievement reinforces Spirit Technologies' ambition: delivering reliable, concrete engineering solutions for major international scientific and industrial programs. Thanks to the synergy between our specialists and CEA researchers, we ensure the technical feasibility and long-term performance of strategic equipment.
As part of the I-HAB project: a major component of the Lunar Gateway space station led by ESA in cooperation with NASA and Thales Alenia Space
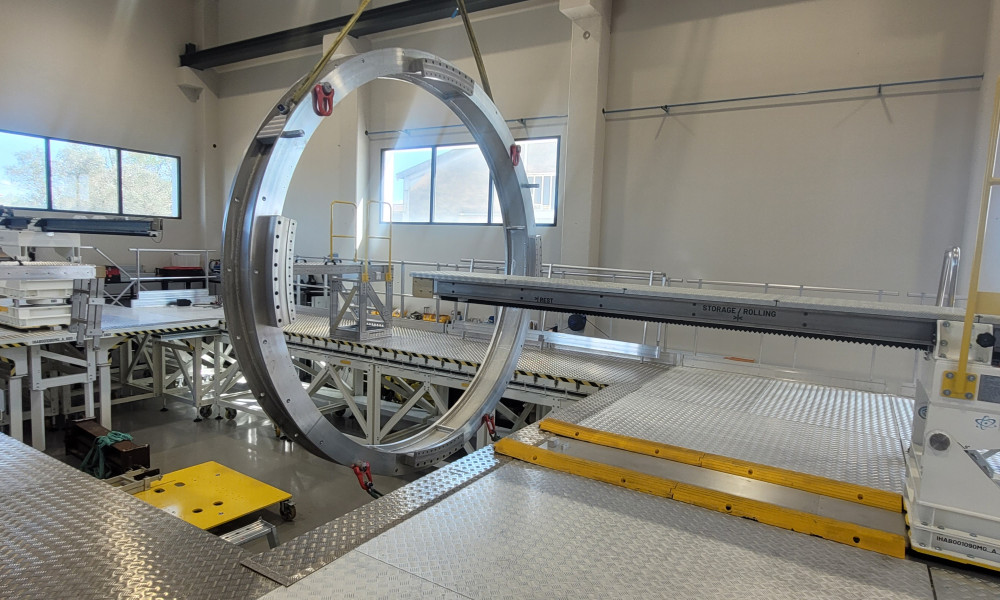
Spirit Technologies designed and developed several MGSEs (Mechanical Ground Support Equipment).
These high-precision mechanical tools are engineered for the complex assembly, handling, and integration operations of a large-scale inhabited space module.
Custom MGSE Solutions for Space Integration
To meet the extreme constraints of critical environments and cleanrooms, the equipment developed by Spirit Technologies' mechanical engineering teams covers the entire operational value chain:
Precise Positioning and Module Support: Ensuring geometric stability and safety during alignment phases.
Secured Handling and Assembly: Incorporating controlled load distribution to protect the critical structures of the I-HAB module.
Ergonomic Operator Access Systems: Platforms and access structures compliant with strict aerospace safety standards.
Dedicated Lifting for Critical Operations: Lifting beams and handling frames engineered for high-value payloads.
A Strong Industrial Partnership for Cutting-Edge Engineering
The development of these MGSE tools relied on close collaboration with an ecosystem of specialized industrial partners. This synergy ensures strict compliance with technical specifications, qualification requirements, and certification standards mandated by international space programs.
This achievement perfectly illustrates Spirit Technologies' ambition: to design, industrialize, and integrate reliable mechanical solutions to meet the challenges of space exploration.
Thanks to our teams' expertise and a field-use-oriented design approach, we support major prime contractors in the aeronautics and space sectors in reaching their most ambitious project goals.